You have no items in your shopping cart.
Choosing a CNC Turning Service is not simply a matter of comparing hourly rates. It is a practical decision about accuracy, communication, materials, lead times, and production risk. A polished website may show impressive parts, yet the real evidence appears in tolerances, inspection records, and repeatable delivery. Ask whether the supplier understands your drawing, material grade, surface finish, and intended operating conditions.
John Saunders, founder of Saunders Machine Works and a respected CNC machining educator, once said, “The best machine is the one that makes you money.” That principle applies directly to outsourcing turned components. The cheapest quotation can become expensive after rework, delayed assembly, or inconsistent batches. A capable CNC Turning Service should explain its equipment, tooling strategy, quality controls, and response to design changes. It should also provide clear answers before production begins.
This guide presents ten practical tips for evaluating a supplier without relying on promises alone. You will see why certifications matter, how to review sample parts, and which questions reveal manufacturing experience. Consider asking for a first-article inspection report. Request realistic tolerances. Discuss packaging, traceability, and communication frequency. Small details matter.
No checklist removes every uncertainty. I have learned that even experienced buyers can overlook delivery assumptions or inspection limits. That weakness deserves attention. A reliable partner welcomes difficult questions, admits constraints, and offers workable alternatives. The right choice is not always the largest factory. It is the service that consistently turns your design into accurate, usable parts.
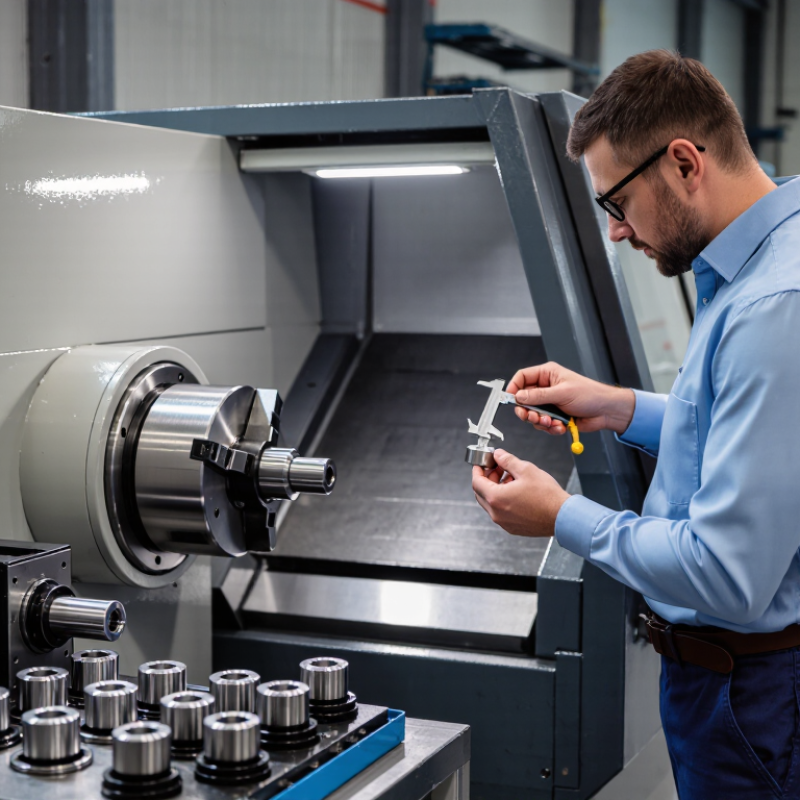
A reliable CNC turning project begins with a clear part definition. State the material grade, stock size, and expected production quantity. Aluminum, stainless steel, brass, and engineering plastics behave differently during cutting. Their hardness affects tool wear, heat, and cycle time. I have seen unclear material notes create avoidable changes after machining starts. Be specific.
Geometry also deserves careful review. Identify diameters, grooves, threads, undercuts, and deep bores on the drawing. Sharp internal corners may require special tooling or design changes. Confirm whether the service can hold the required length-to-diameter ratio. Complex profiles often need additional inspection points. A simple sketch is not enough.
Tips: Write critical dimensions directly on the drawing. Separate functional tolerances from general tolerances. Ask how measurements are verified, especially for small bores and threaded features. Surface finish should include a measurable value, such as Ra, rather than “smooth.” Mention sealing areas, sliding surfaces, and visible faces. These details guide machining and inspection decisions.
Tolerance choices should match the part’s real function. Extremely tight tolerances can increase cost without improving performance. That is easy to overlook. Request a manufacturability review before approval. Discuss datum references, burr limits, edge breaks, and finish consistency. One missing note can affect fit, appearance, and assembly reliability.
Choosing a CNC turning service begins with verifying machine capability against your ±0.005 mm tolerance requirements. Do not rely on a general accuracy statement. Ask for documented repeatability, positioning accuracy, and recent inspection records. A machine may achieve tight tolerances briefly, then drift as temperature changes. That detail matters.
Tip: Request a sample inspection report from a comparable turned part. Check whether measurements were taken with calibrated micrometers, gauges, or a coordinate measuring machine. Ask about measurement uncertainty, not only the final numbers. Reliable suppliers should explain their process clearly. Short answers can hide problems.
Tip: Discuss material, diameter, length, and workholding before approval. Stainless steel may heat differently from aluminum during extended cutting. Chucks, collets, and worn tools can also affect concentricity. Confirm how the shop controls thermal growth during production. A climate-controlled inspection area is useful, but it cannot correct poor machining.
In practice, I would request a first-article inspection before releasing a larger batch. Review actual dimensions, surface finish, thread quality, and runout. Confirm the inspection method matches the drawing. One overlooked datum can invalidate an otherwise accurate report. I have seen tolerance plans fail because the setup was rigid, but the measurement reference was wrong. That mistake is easy to miss. Ask who approves corrective actions when results approach the tolerance limit. A capable service should welcome that question.
Reference tolerance and measurement-resolution levels for evaluating precision CNC turning suppliers.
A ±0.005 mm dimensional requirement represents a total tolerance zone of 0.010 mm. When reviewing a CNC turning service, confirm that the machine, tooling, fixturing, process stability, and inspection equipment can consistently support this requirement. A measurement resolution of approximately 0.001 mm is commonly selected for reliable verification, while actual capability should be demonstrated with documented trial-part data and calibrated instruments.
Choosing a CNC turning service requires more than comparing hourly prices. Ask how the supplier controls quality from quotation through final shipment. ISO 9001 certification shows that documented processes exist, but it does not guarantee perfect parts. Request the current certificate and confirm its scope covers CNC machining. Then ask how operators handle drawing revisions, material certificates, and nonconforming parts.
Inspection data reveals the real process. Request a sample inspection report for a similar turned component. It should identify dimensions, tolerances, gauges, equipment, and measurement results. Look for calibration dates and clear links between results and part numbers. Useful suppliers can explain their sampling plan and process capability data. Statistical process control can show whether a diameter is drifting before parts fail inspection. Ask for first-article inspection when the design is new.
Do not accept polished reports without questions. I once reviewed a report with every dimension marked “pass,” yet no measurement method was listed. That gap mattered. Ask whether critical features receive independent verification, such as coordinate measurement or calibrated micrometers. Also examine how inspection records are stored and retrieved. Fast access supports traceability during a defect investigation. A reliable service should discuss corrective actions with evidence, not vague promises. One warning sign is repeated rework without documented root-cause analysis. Quality systems need people, not paperwork alone. A short factory visit can reveal whether inspection tools are clean, labeled, and actually used. Expect some process variation. The key is controlled variation, supported by consistent data.
Choosing a CNC turning service means comparing more than hourly rates. The 2024 State of Smart Manufacturing report surveyed 1,560 manufacturers. It found that 95% had invested, or planned to invest, in smart manufacturing. Digital quoting helps, but it cannot replace engineering judgment. Ask for a realistic lead-time range, not a best-case promise. Request dates for programming, material arrival, first-article inspection, and production. In practical shop-floor work, material delays often matter more than cutting time.
Batch size changes the economics. A prototype may carry setup and inspection costs that disappear across 500 parts. Larger orders can still expose capacity limits. Ask whether your batch runs together, uses multiple machines, or ships in scheduled lots. A 2024 manufacturing workforce study found that 77% of employers struggled to attract and retain workers. Capacity claims deserve verification. Ask for recent on-time performance, not vague confidence. Small detail. Big difference.
Pricing should separate material, tooling, setup, machining, finishing, inspection, packaging, and freight. DFM support should flag thin walls, deep bores, tight tolerances, and excessive surface finishes. NIST reports that small and medium-sized manufacturers represent about 99% of U.S. manufacturing firms. Practical engineering support can strongly affect smaller projects. I still question one assumption: the lowest quote is cheapest only when revisions remain unlikely. Share the drawing, 3D model, tolerance table, annual volume, and deadline. Compare like with like.
| Tip | Decision Area | What to Compare | Useful Questions to Ask | Potential Red Flags |
|---|---|---|---|---|
| 1 | Confirm machine capability Equipment fit | Check turning diameter, part length, spindle capacity, live tooling, bar feeding, and available secondary operations. Typical CNC lathes cover small precision parts through larger shafts, but capacity varies significantly by machine. | Can the shop produce the required diameter, length, thread, groove, bore, and tolerance in one setup? Is a sub-spindle or live tooling capability needed? | The supplier cannot state machine limits, proposes multiple setups without explaining the impact, or accepts the drawing without reviewing difficult features. |
| 2 | Compare lead times Schedule | Separate quotation time, first-article time, production lead time, inspection time, and shipping time. Prototype work may take several business days to a few weeks; repeat production is often planned separately. | What is the promised date for first parts and the full batch? When does the lead time start? Are material purchasing, programming, inspection, and finishing included? | Only a broad promise such as “fast delivery” is provided, or the quoted lead time excludes material procurement and quality inspection. |
| 3 | Match batch size Volume | Confirm minimum order quantities, prototype support, repeat-order capacity, and monthly output. One-off parts and high-volume work may require different equipment, tooling, and pricing models. | Can the supplier handle one prototype, a pilot batch, and scheduled production? How are setup costs distributed between small and large quantities? | The supplier is optimized only for mass production, refuses small batches, or provides no plan for scaling after prototype approval. |
| 4 | Evaluate total pricing Cost | Compare the complete landed cost: material, programming, setup, machining, tooling, deburring, inspection, finishing, packaging, and freight. Unit price normally decreases as setup costs are spread across more parts. | Which costs are included in the unit price? Are tooling, fixtures, certificates, surface treatment, packaging, and shipping listed separately? | A very low unit price excludes essential operations, has unclear assumptions, or changes substantially after the drawing and material are reviewed. |
| 5 | Review DFM support Engineering | Strong DFM support should identify unnecessary tight tolerances, difficult internal features, poor tool access, thin walls, deep bores, sharp corners, and inefficient setups before production. | Is drawing review included? Will the supplier suggest tolerance changes, standard tool sizes, radius changes, or a different machining sequence while preserving function? | The quote is issued without technical feedback, or the supplier recommends changes without explaining functional, cost, or performance effects. |
| 6 | Verify tolerance control Precision | Compare achievable tolerances for critical diameters, concentricity, runout, threads, and surface finish. General tolerances should not be treated as a substitute for specifically marked critical requirements. | Which dimensions are inspected on every part? What measuring equipment is used? Can the supplier provide capability data or a first-article inspection report? | The supplier guarantees every tolerance without reviewing geometry, material, quantity, or inspection method. |
| 7 | Check material traceability Materials | Confirm the exact grade, condition, heat treatment, and required material certificates. Common turning materials include aluminum alloys, steels, stainless steels, brass, copper alloys, and engineering plastics. | Can the supplier provide a material certificate and lot traceability? Are substitutions allowed, and who must approve them? | The material is described only as “steel” or “aluminum,” certificates are unavailable, or substitutions are made without written approval. |
| 8 | Assess quality systems Inspection | Review calibration practices, in-process inspection, final inspection, nonconformance handling, sampling plans, and documentation. Requirements should match the risk and application of the component. | What inspection report is included? Are gauges calibrated? How are nonconforming parts contained, investigated, and corrected? | Inspection is performed only by visual check, measuring equipment has no calibration records, or quality records cannot be supplied when requested. |
| 9 | Confirm finishing and assembly Completion | Determine whether the supplier manages deburring, cleaning, heat treatment, plating, anodizing, passivation, coating, marking, and assembly through qualified internal or external resources. | Who controls outside processing? Are color, thickness, hardness, cleanliness, and cosmetic standards documented and inspected? | Finishing is outsourced without traceability, cosmetic acceptance criteria are undefined, or the final delivery date excludes outside processing. |
| 10 | Test communication and continuity Reliability | Evaluate quotation clarity, engineering response time, revision control, production updates, packaging standards, and the ability to support repeat orders with consistent settings and documentation. | Who is responsible for technical communication? How are drawing revisions controlled? Can approved programs, inspection records, and process notes support future orders? | Different contacts provide conflicting information, revisions are tracked informally, or the supplier cannot explain how repeat-order consistency is maintained. |
Note: Lead times, achievable tolerances, production quantities, and prices depend on part geometry, material, quantity, finish, inspection requirements, and shipping location. Request a drawing-based quotation for an accurate comparison.
Choosing a CNC turning service requires more than comparing hourly prices. Ask which certifications their quality system holds and whether the certificates are current. Request sample inspection reports, calibration records, and process-control documents. A serious supplier should explain how operators verify diameter, thread pitch, surface finish, and concentricity. Small details matter.
Traceability should follow every part from material receipt to final shipment. Check whether the service records heat numbers, machine IDs, operator names, inspection results, and revision levels. A labeled batch traveler or digital record can prevent costly confusion. Ask how nonconforming parts are isolated. During a factory review, inspect storage areas, not just polished production lines. Reality is often less tidy.
Data security deserves equal attention. Confirm access controls, file encryption, revision management, and employee confidentiality procedures before sharing sensitive drawings. Ask how files are deleted and whether subcontractors can access them. After-sales service should include clear response times, root-cause analysis, replacement procedures, and technical communication. Test the process with a practical question. Slow or vague replies reveal risk. I once focused too heavily on machining accuracy and overlooked response speed. That mistake delayed a production release. A capable partner should support corrective actions after delivery, not disappear when the invoice is paid.